Choosing a CNC press brake is less about peak tonnage on a spec sheet and more about the bends you run every week. Bed length, material mix, flange accuracy, tooling and control decide whether an affordable torsion bar machine is enough — or whether premium multi-axis CNC pays back on your nest. Size to everyday work first, then pick the control class.
Size tonnage and bed length to the bends you form regularly, then choose the control class. Compare Rhino torsion bar and Rhino Premium CNC, then use the tonnage guide.
Size to everyday bends, then pick the control class
- List your longest and heaviest routine bends — not one-off peaks — then match bed length and tonnage with a safety margin.
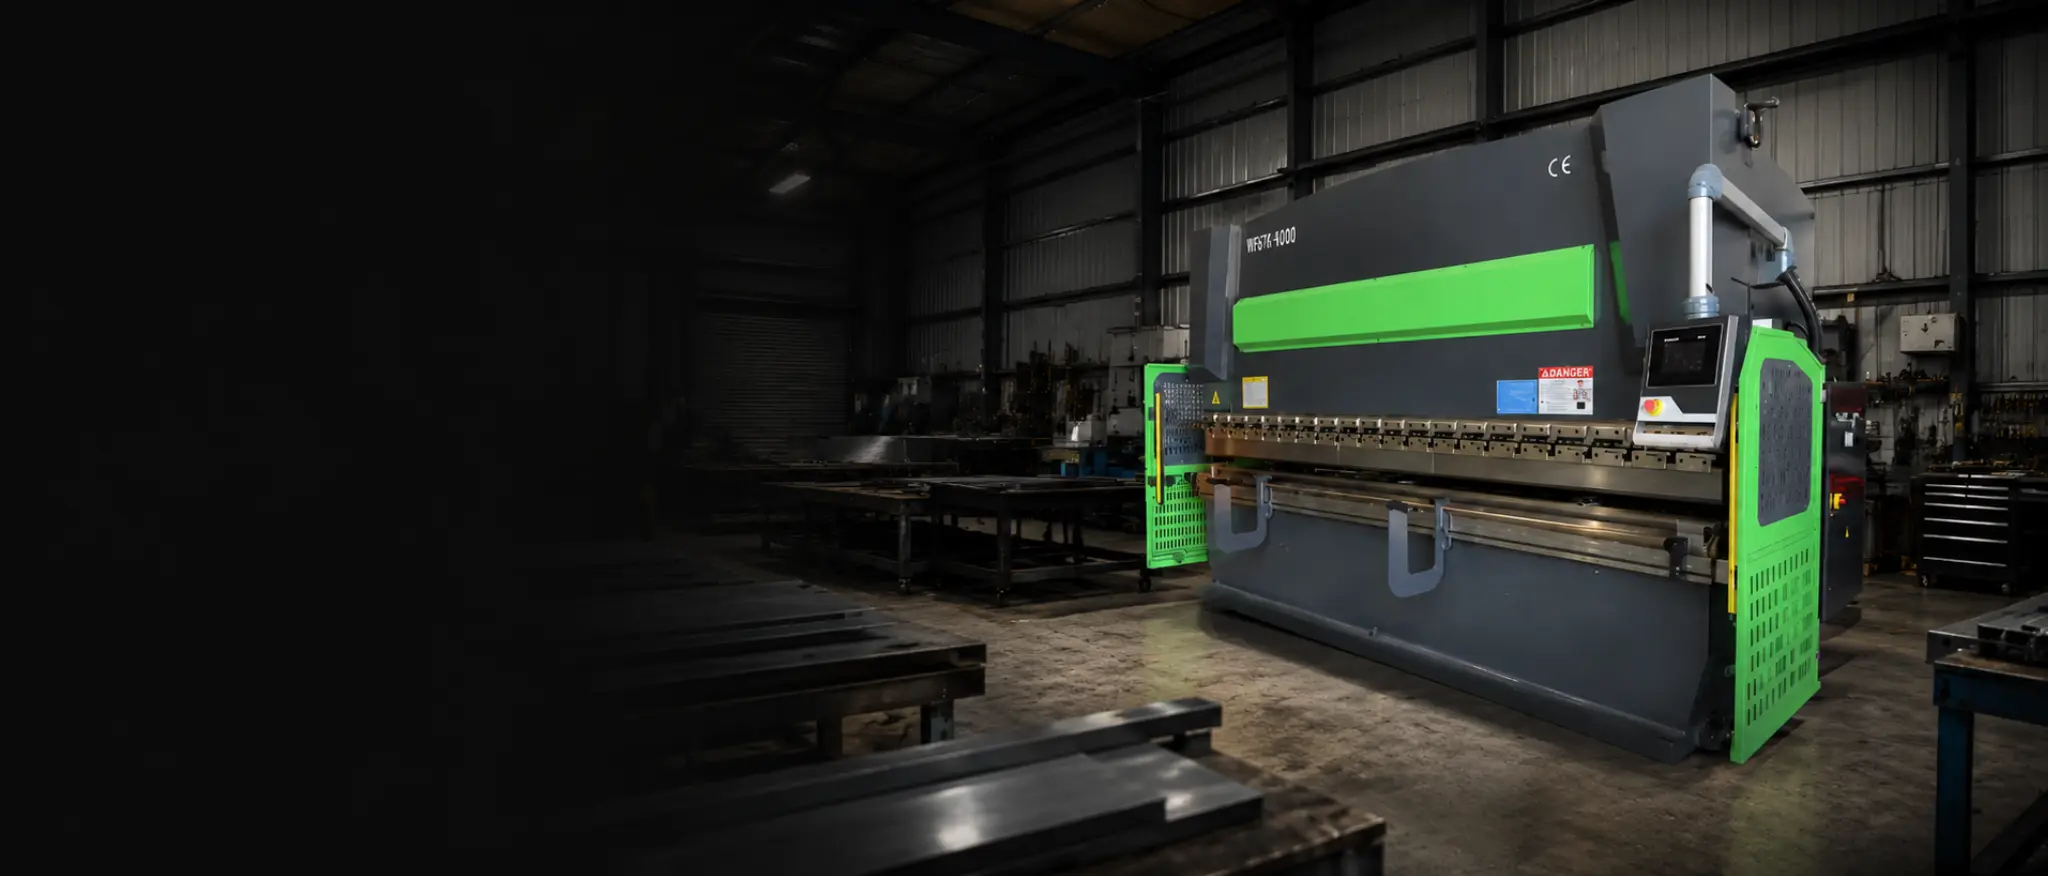
- Everyday mild-steel flanges and simple backgauge work often suit Rhino torsion bar CNC with Delem DA-41T.
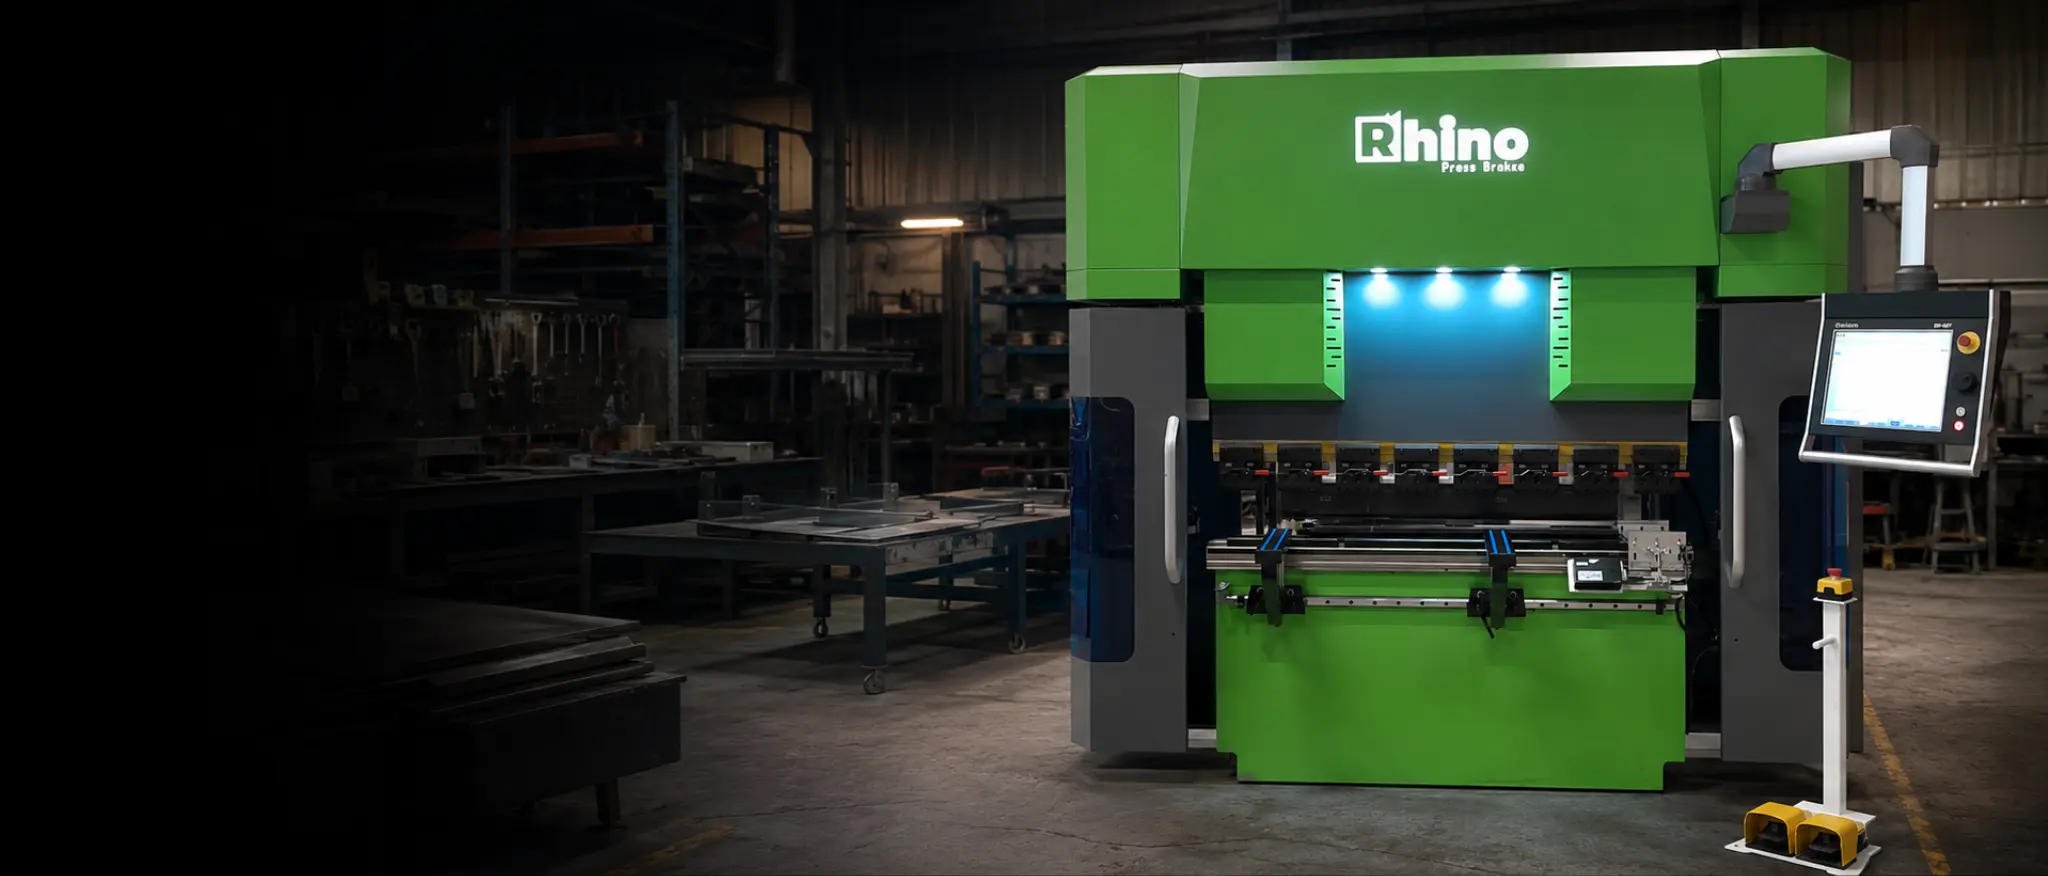
- Tighter angles, complex flanges and higher axis counts push toward Rhino Premium CNC with DELEM multi-axis control and Lazersafe.
- If box-and-pan folding dominates — or you only need straight blanks — compare hydraulic folders and guillotines before you overspec a brake.
Browse Rhino torsion bar press brakes and Rhino Premium CNC press brakes. Sanity-check force and V-die choices on the press brake bending calculator before you shortlist.
Start with tonnage and bending length
Tonnage is the force the beam can apply. Bending length is how much bed you have for the bend line. Undersize either and you reject jobs or overload tooling. Oversize both and you pay for capacity that sits idle. Size to the longest everyday panel and the thickest routine material — then leave headroom for stainless and longer hits.
- Estimate air-bending force from material, thickness, bend length and V-die opening — then compare to machine-rated tonnes and tonnes-per-metre tooling limits.
- Confirm the bed covers your longest flange programmes without awkward repositions on every nest.
- Remember stainless typically needs more force than mild steel at the same thickness; aluminium often needs less.
- Document material, thickness, V opening and estimated tonnage on internal quotes so demos match real work.
Read the press brake tonnage guide for material strength, V opening and tonnes per metre, then use the bending calculator for air-bending estimates. Treat the result as a planning check — tooling charts and test bends remain the final reference.
Torsion bar or premium CNC
Mantech supplies two Rhino press-brake families. They are not the same machine class. Picking the wrong one is the most common buying mistake after underestimating bed length.
| Factor | Torsion bar CNC (Rhino W67Y) | Premium CNC (Rhino Premium) |
|---|---|---|
| Typical buyer | Workshops needing accurate, affordable CNC bending | Production cells needing multi-axis accuracy |
| Control | Delem DA-41T touchscreen — Y + X backgauge | DELEM CNC with higher axis options (3+1 to 8-axis families) |
| Hydraulics / build | Torsion bar synchronisation for everyday production | Bosch-Rexroth hydraulics · monoblock precision platforms |
| Safety package | Standard industrial guarding for the range | OEM-embedded Lazersafe + interlocked fencing options |
| Best everyday fit | Mild steel flanges, brackets, enclosures, general fab | Complex flanges, crowning control, higher repeat accuracy |
| Where to compare | Rhino torsion bar hub | Rhino Premium CNC hub |
For the full class decision, read torsion bar vs CNC press brake. Range detail lives on the torsion bar hub and premium CNC hub.
Tooling, Euro clamping and setup time
A press brake without the right punch and die set is a slow machine. Euro-style tooling and quick-release clamping cut changeovers when your mix jumps between flanges. Plan tooling inventory alongside tonnage — narrow V-dies raise force quickly; wider openings ease tonnage but grow inside radius and minimum flange.
- Confirm Euro tooling / quick-release clamping is included or quoted for your range.
- Match V-die openings to everyday thicknesses — not only the thickest plate you might ever bend.
- Check punch and die tonnes-per-metre ratings separately from machine peak tonnage.
- Ask how tool libraries and bend programmes are stored on the CNC for multi-operator shops.
Rhino torsion bar machines ship with Euro tooling as standard on the press brakes hub. Premium platforms add European quick-release and intelligent tool management on the premium hub.
Safety, install and support
Press brakes need guarding discipline, trained operators and a floor plan that allows blank handling. Premium cells often add Lazersafe light-curtain style protection in the bending zone. All installs still need space for sheet staging, scrap and safe approach. Budget installation, commissioning and operator training — not only the machine invoice.
Mantech supplies, installs and trains from Halesowen — see press brake installations and the Kes Power & Lighting case study for a 100T torsion brake in electrical manufacturing.
When a folder or guillotine fits better
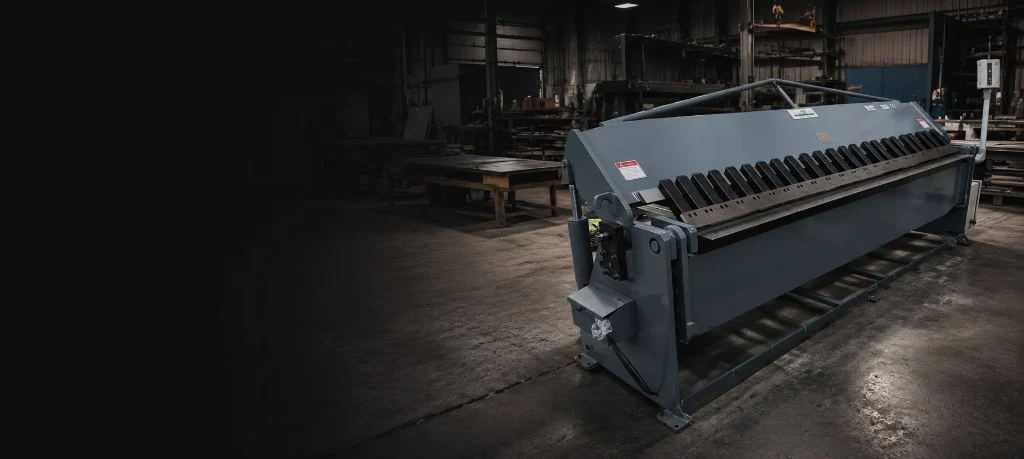
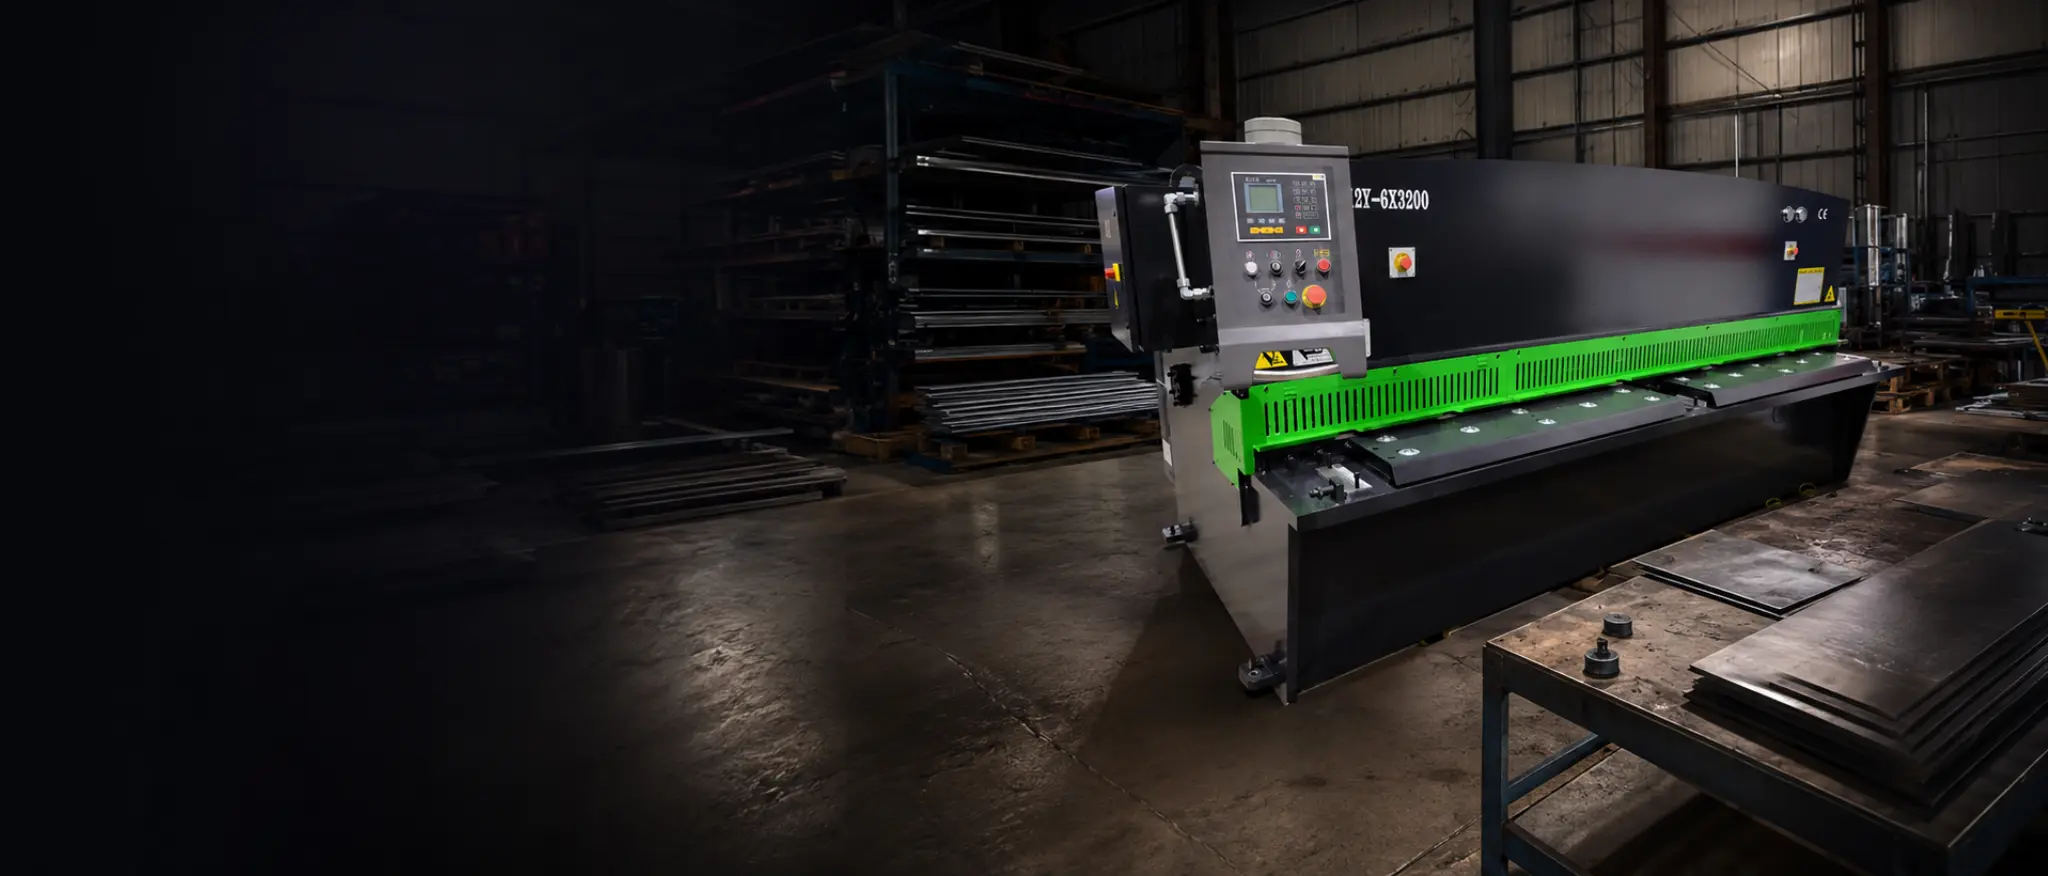
Not every forming job needs a press brake. Hydraulic folders excel at box-and-pan work with segmented tooling. Guillotines own straight blanking before the bend cell. Many shops run shear plus brake as a pair — and add a folder when pan work dominates.
- Straight blanks and guillotine capacity first — size shear before you overspec the brake.
- Box, pan and segmented folding without a full brake cell — a hydraulic folder may be the better first former.
- Laser-cut nests feeding a bend cell — align press-brake bed length with everyday nest sizes on the cutting programme.
When the forming work is mostly boxes and trays, start with press brake vs hydraulic folder. The hydraulic folder range and industrial guillotines are there if you already know which machine you need.
Buying checklist before you quote
- List top five jobs by material, thickness, bend length and flange complexity.
- Estimate tonnage and V-die needs on the bending calculator — then add a safety margin for stainless.
- Decide torsion bar CNC vs premium multi-axis based on accuracy and axis count — not price alone.
- Confirm Euro tooling, control programmes, guarding and training are in the package.
- Check whether a guillotine or folder should sit alongside the brake in the same cell.
- Bring sample drawings and scrap to a demo so angle and flange accuracy are judged on your work.
Explore Mantech CNC press brakes
Mantech supplies Rhino torsion bar and Premium CNC press brakes from Halesowen with UK installation, commissioning and operator training. If you are replacing a failed brake, bringing bending in-house, or pairing a new shear with a bend cell, our engineers can map tonnage, bed length and control class to your everyday work.
Compare torsion bar press brakes and premium CNC press brakes, plan force on the bending calculator, or call the team — UK 0121 541 1444 · Ireland (+353) 83 804 8820. Browse UK installs on installations.
Useful next reads
- Torsion bar vs CNC press brake
Sync, axes, accuracy and who should buy which.
- Press brake bending calculator
Estimate tonnage, V-die opening and flange geometry before you shortlist.
- Rhino torsion bar press brakes
Affordable CNC bending range — Delem DA-41T and Euro tooling.
- Rhino Premium CNC press brakes
Multi-axis DELEM platforms when accuracy and crowning matter.
- Press brake vs hydraulic folder
When box and pan work should sit on a folder instead of a brake.
Frequently asked questions
How do I know what press brake tonnage I need?
Start with the material, thickness, bend length and V-die opening for your regular jobs. The press brake tonnage guide explains each input and the separate tooling limit. Use the bending calculator for the estimate, then confirm it against the machine and tooling charts.
What bed length should I buy?
Cover your longest routine bend line with room to stage parts safely. Buying only for a rare oversized panel often wastes capital. Undersizing forces constant repositioning. Match bed length to your cutting nest sizes when laser and brake share a cell.
Torsion bar or premium CNC press brake?
Torsion bar CNC with Delem DA-41T suits many shops doing accurate everyday flanges on a controlled budget. Premium CNC earns its place when multi-axis backgauge, crowning and tighter angle repeatability drive your quoting. Read the torsion bar vs CNC press brake guide for the full class decision.
Do I need Euro tooling included?
Euro-style punches and dies with quick changeovers keep mixed flange programmes productive. Confirm what tooling ships with the machine, what is optional, and how tool libraries are stored on the CNC for multi-operator teams.
Should I buy a press brake, folder or guillotine first?
If you lack straight blanking capacity, a guillotine or laser may come first. Box and pan work can favour a hydraulic folder — that choice is covered in the press brake vs hydraulic folder guide. A CNC press brake is the forming machine for general flanges. Map the work you do every week, then shortlist.